~ Fixed Head Turning: Capabilities, Tolerances and Best Use Cases ~

Jake Hughes • October 1, 2026

Key Highlights


  • Fixed head turning uses CNC lathes with a main spindle held in a fixed position during the turning process.
  • It suits short workpieces, larger diameter parts, and jobs needing stable machine tools for high-precision output.
  • Rotec Aerospace Limited in Evesham, UK, operates fixed head machines with automation for repeatable production.
  • Live tooling supports different operations such as milling, drilling, grooving, and cross drilling on complex shapes.
  • Tight tolerances depend on setup, material, tooling, and inspection, not one factor alone.
  • Fixed head turning is widely used across aerospace, motorsport, rail, oil and gas, and industrial sectors.


Introduction


Fixed head turning remains a core turning process for precision parts made on CNC lathes. It gives stable support, strong cutting performance, and a practical route to high-precision components across many industry sectors. At Rotec Aerospace Limited, this method supports both prototype work and repeat production in an automated facility near the M5 in Evesham, UK. To choose the right manufacturing operation, you need to understand how fixed head turning works, where it fits best, and what affects achievable results.

Quick Answer: What Is Fixed Head Turning, and Who Is It For?
What Is Fixed Head Turning, and Who Is It For?

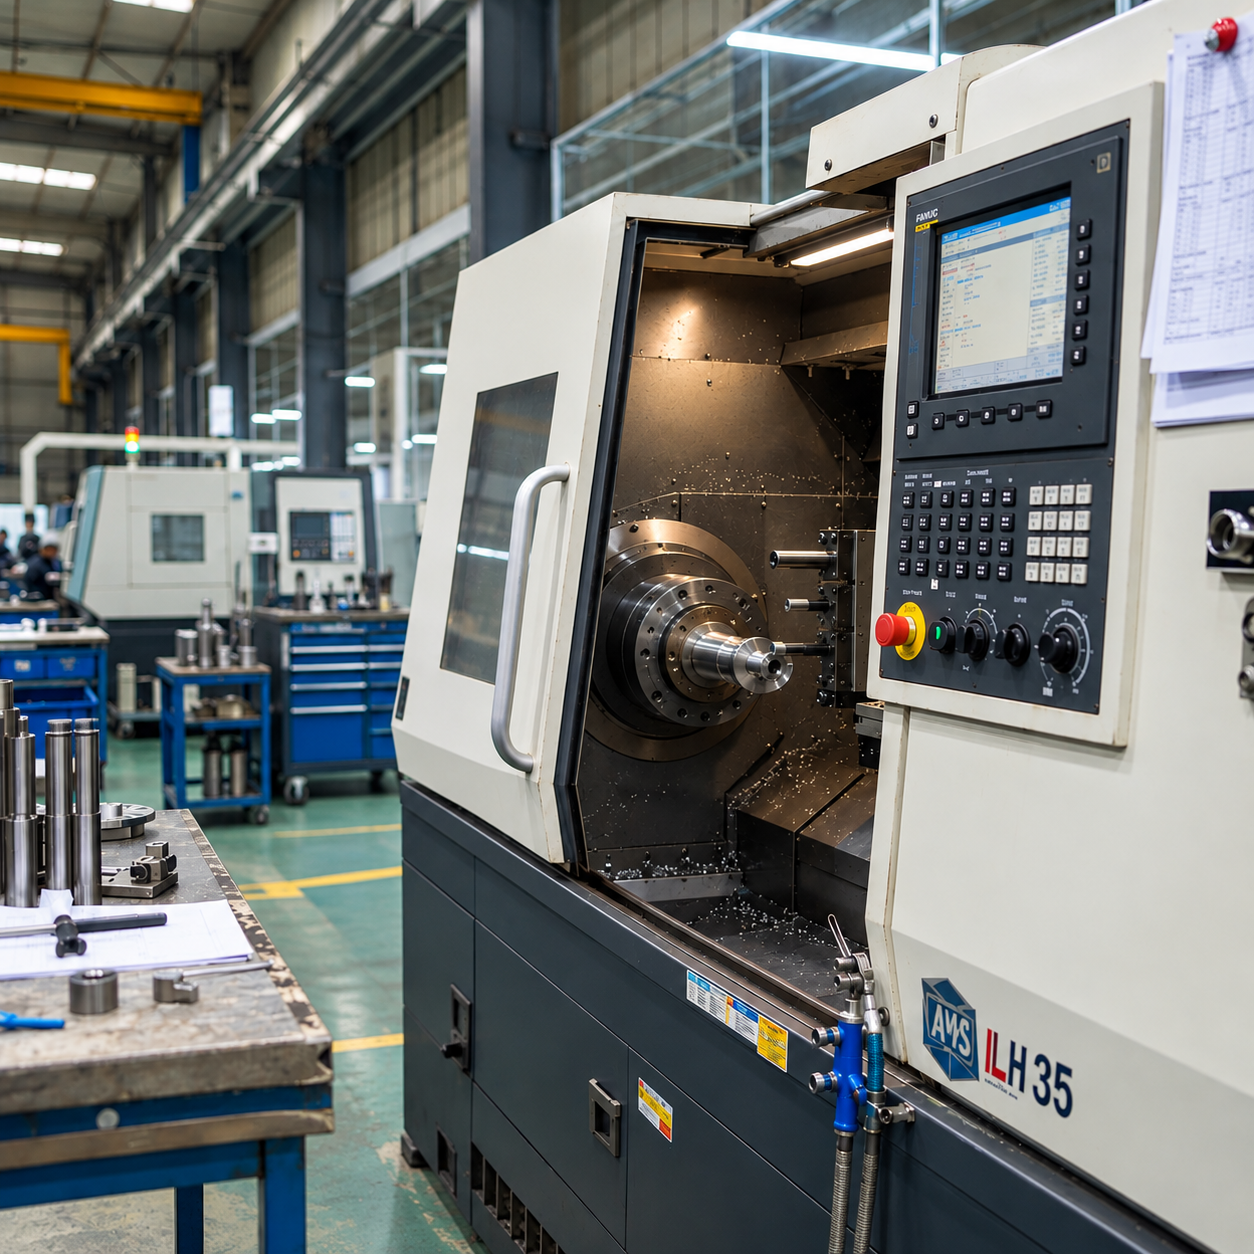
Fixed head turning is CNC turning in which the main spindle remains in a fixed position while the workpiece rotates and the cutting tool moves to create the required form. This setup is used to machine short workpieces, larger diameter components, and many complex parts where rigidity and stable cutting matter. It is a common choice for precision engineering because it supports efficient stock removal and good control of dimensions.


In practice, fixed head turning suits customer requirements such as low-volume prototype batches, high-volume small-turned parts, die-making consumables, bolts, fasteners, heatsinks, shafts, pins, and aerospace components. It is also useful when rough bar stock or billets are involved. If your part is relatively short for its diameter and needs several operations on one machine, fixed head machining is often the right starting point.


Key Takeaways: Fixed Head Turning in CNC Machining


Fixed head turning offers a strong balance of flexibility, control, and productivity on CNC lathes. Because the process uses numerical control, it can produce repeatable features across prototype and batch work. It is especially useful for short workpieces, parts with larger diameters, requirements, and jobs that need several machining steps completed with one setup. For many applications, this helps reduce handling and supports better turnaround times.


Another key point is that performance depends on the full process, not only the machine. Cutting tool choice, workholding, material behavior, and inspection all affect the final result. Fixed head machines are also well suited to large stock removal and a broad range of materials. At Rotec, automation and unmanned running add production efficiency, while CMM inspection supports verification for customer requirements across demanding sectors.


Defining Fixed Head Turning in CNC Precision Engineering

Fixed head turning is a CNC turning method where the headstock stays stationary and the raw material rotates in the spindle while tools machine the part. In simple terms, it is a turning process built for controlled cutting on parts that do not need sliding head support. That makes it a practical option for many high-precision components.


You will often see fixed head machining used where the part is short, comparatively rigid, or made from rough bar stock or billet. It handles a wide range of diameters and materials, which is why it remains a standard choice in precision engineering. The next sections explain the setup and the key differences from sliding head technology.


Fixed Head Turning Explained: How the Process Works

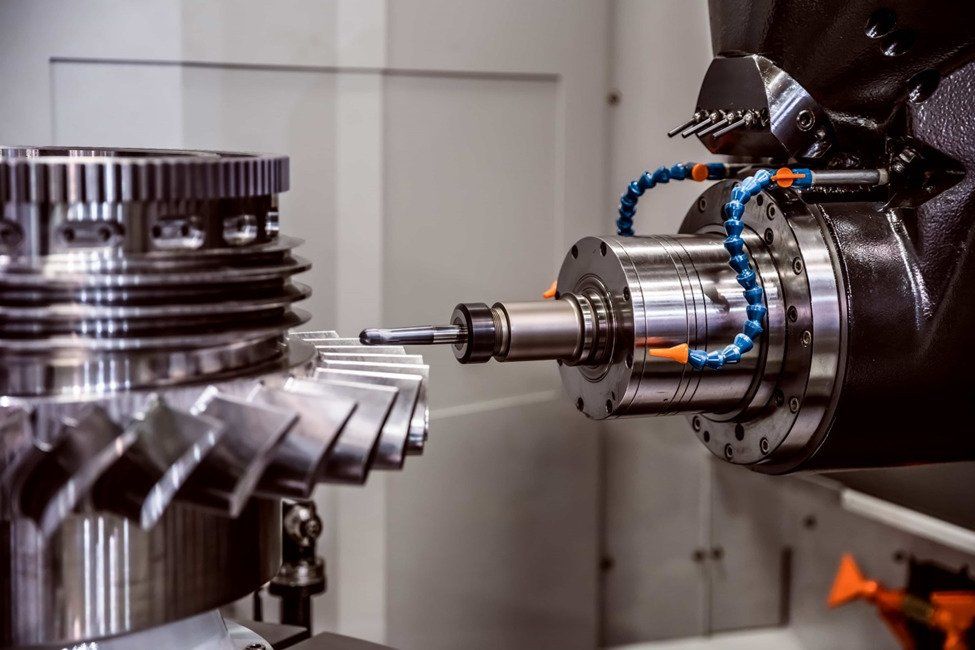
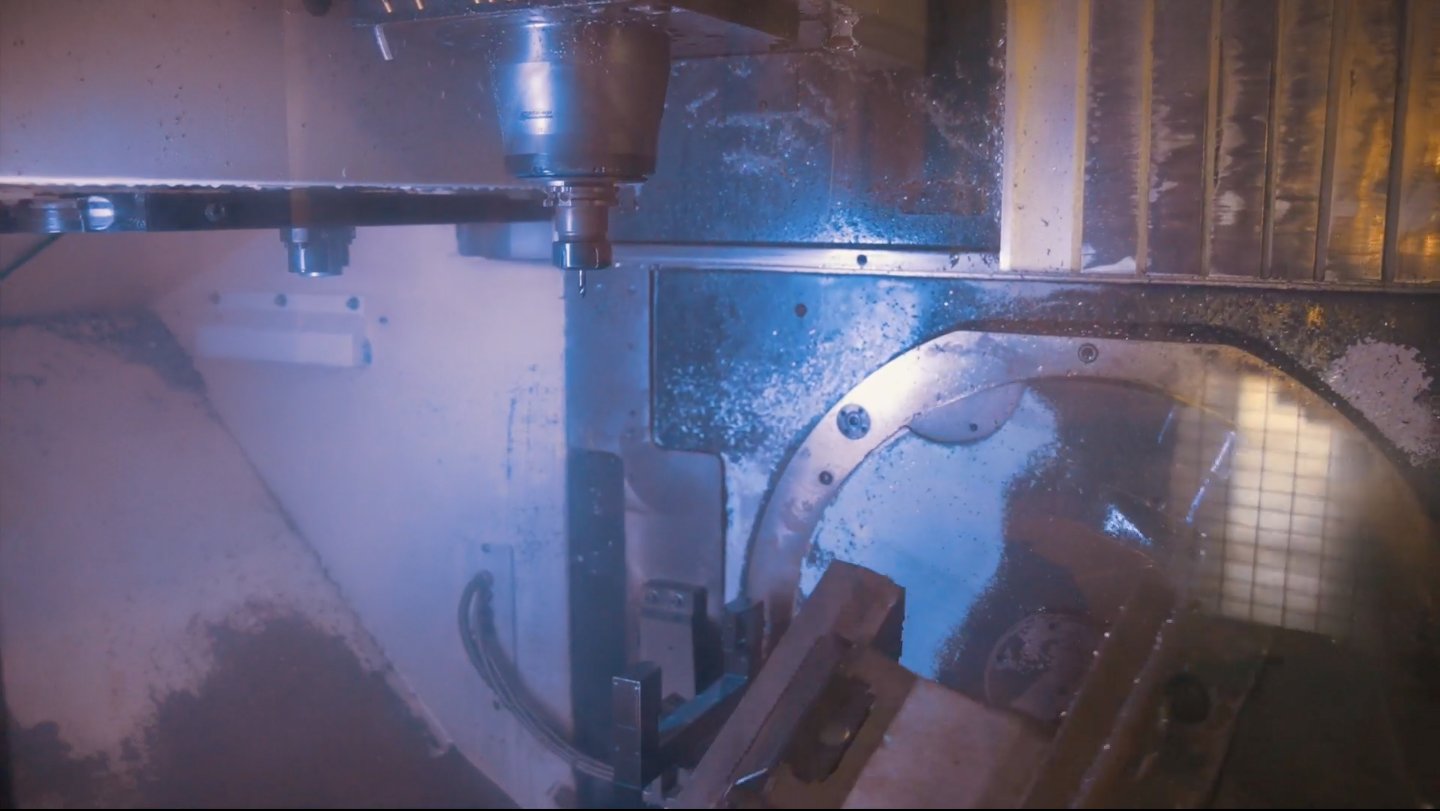
A fixed head-turning center works by holding the workpiece in the main spindle while the headstock stays in a fixed position. The spindle rotates the material, and the cutting tools move around it to remove material in a controlled way. This is how machine tools create high-precision cylindrical and prismatic features.


The basic setup process usually follows these steps:

  1. Load the bar, billet, or blank into the spindle or chuck.
  2. Secure the workpiece and confirm the datum.
  3. Fit the required tools for turning, drilling, or milling features.
  4. Run the CNC programme and check the first-off part.


Once the programme is proven, the machine can repeat the cycle with strong consistency. Live tooling and sub-spindle capability on suitable machines can add more stages in one setup, helping produce complex shapes with fewer manual interventions. That is one reason fixed head turning stays effective for both development parts and repeat orders.


Fixed Head Turning in Context: A Comparison with Sliding Head Technology

The key differences between fixed-head lathes and sliding-head machines come from how the material is supported during machining. In fixed head turning, the spindle position stays fixed, and the workpiece is machined from that held point. In sliding head machining, the headstock moves, and a guide bush supports the bar close to the cut, which helps with long, slender parts.


Here are the main distinctions:

  • Fixed head machines are better suited to short workpieces, rough bar stock, billets, and larger diameters.
  • Sliding head machines are stronger for high-precision turning of small diameters and long parts with a high length-to-diameter ratio.
  • Dimension limits differ because sliding head machines rely on guide bush support and are limited by maximum bar diameter.


As a simple rule, choose a fixed head for shorter, stiffer components and a sliding head for long, narrow ones. Machine tool companies have broadened the overlap between both technologies, but the basic selection logic still matters. Rotec offers both approaches, so the choice can be matched to actual part geometry and customer requirements.


Capabilities of Fixed Head Turning at Rotec Aerospace Limited
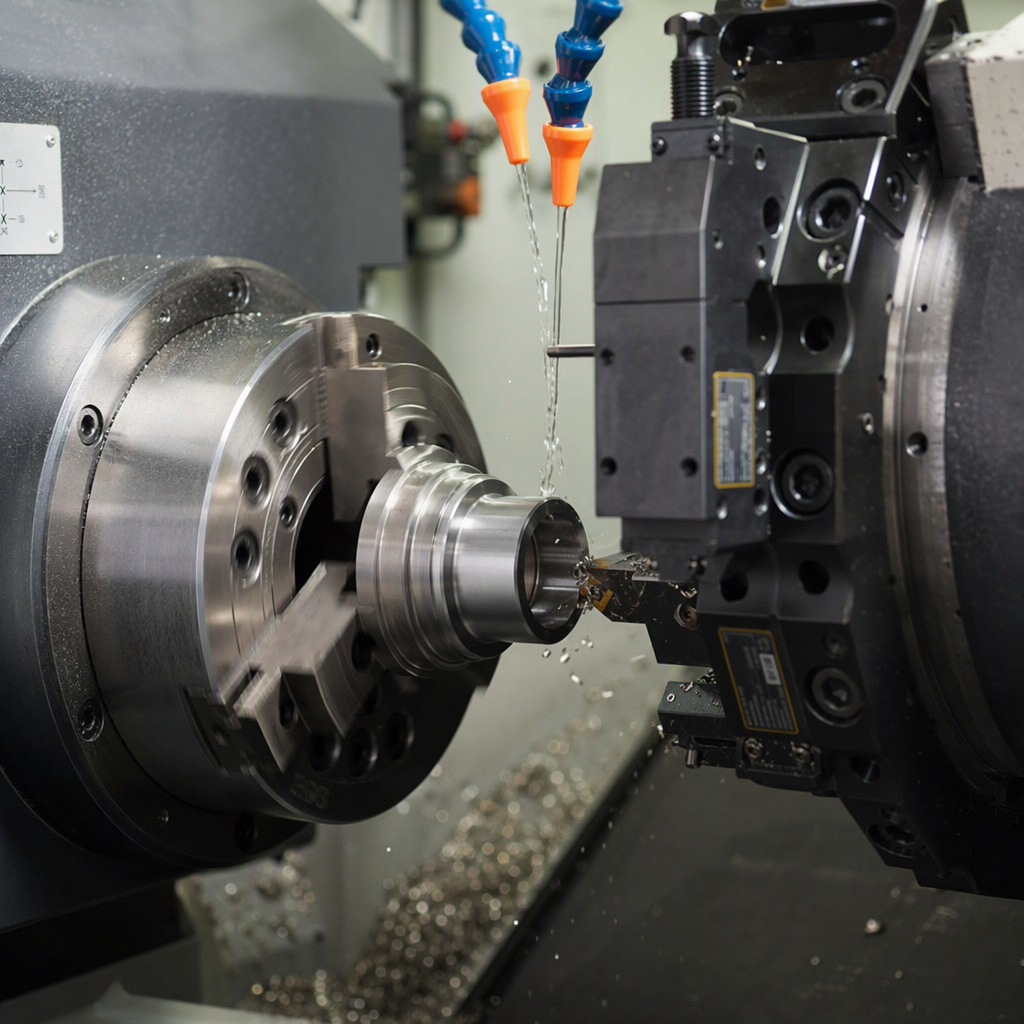
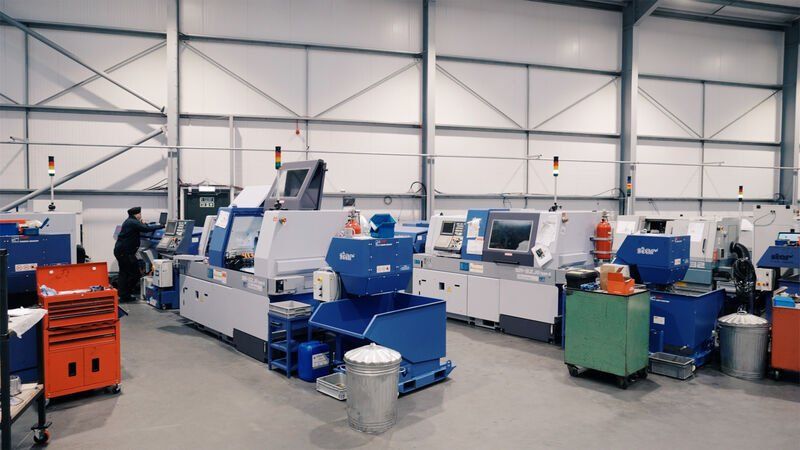
Rotec Aerospace Limited operates fixed-head machine tools that support both flexible production and repeat manufacturing. These CNC lathes are used for turning work across sectors such as aerospace, space and satellite, Formula 1, military, oil and gas, automotive, agricultural, industrial, and rail. This makes fixed head capacity an important part of Rotec’s one-stop shop offering in Evesham, UK.


Just as important, the facility runs 24/5, and many machines operate unmanned. That level of automation supports efficient throughput, especially for repeat work and high-volume small-turned parts. The next two sections cover the machine platforms, automation features, and the range of supported operations in more detail.


Machine Types and Automation Features

Rotec’s fixed-head CNC lathes include a strong mix of machine tools for different production needs. The installed machines are

  • DMG MORI NLX 2500 / 700 (x2)
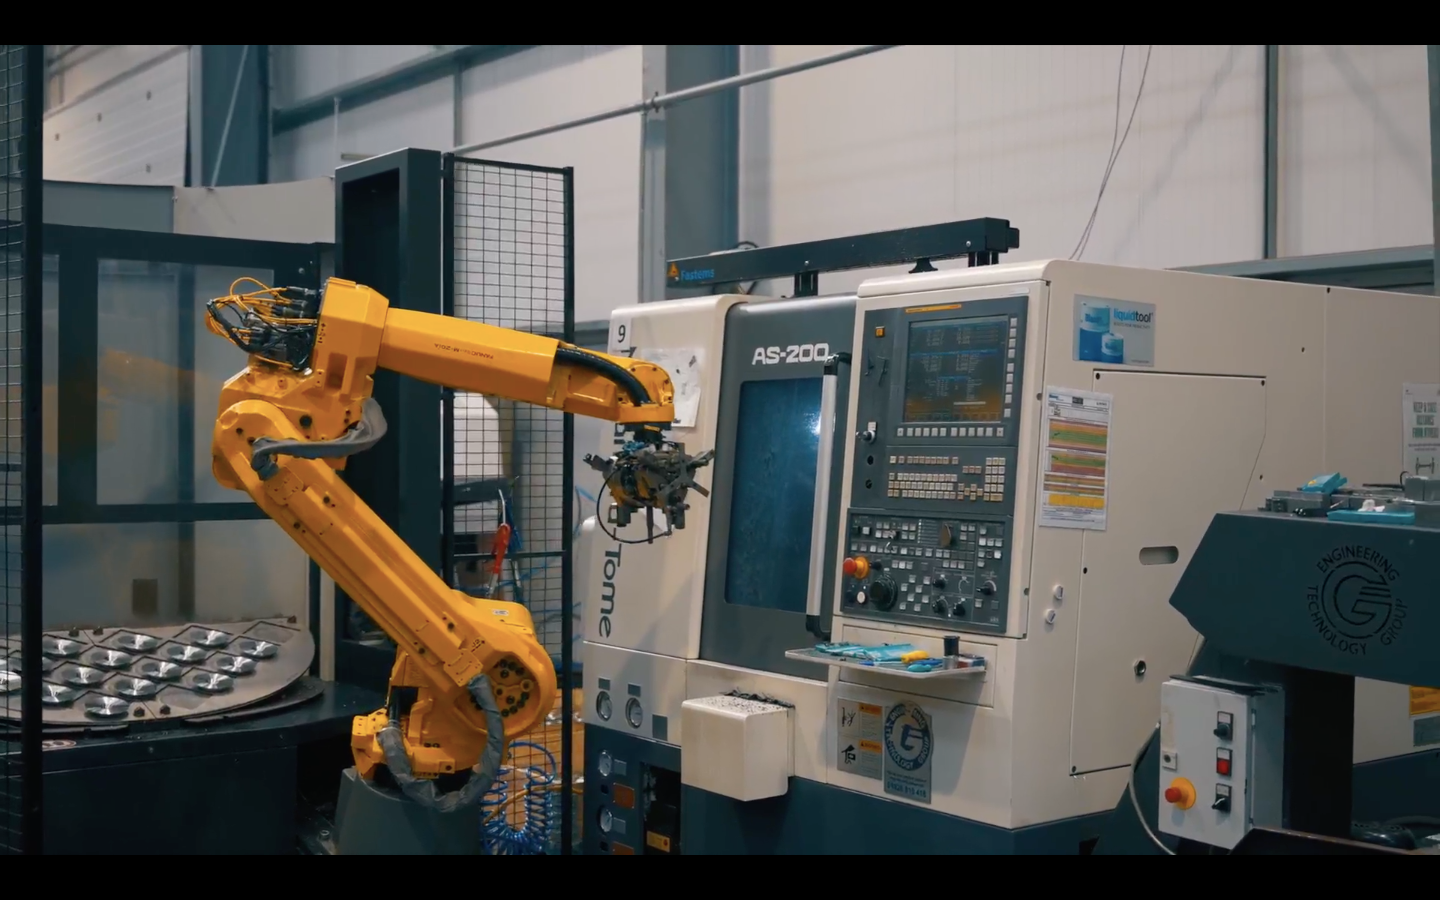
  • Nakamura AS200 with Halter robot loading cell
  • Nakamura NTRX300 with Halter robot loading cell (x2)
  • Nakamura NTY-3 (x2)


These platforms support both standalone turning and more advanced mill/turn work. Robot loading on the Nakamura AS200 and Nakamura NTRX300 systems adds automation for repeat batches and helps keep utilization high. In a 24/5 facility, that matters for productivity, consistency, and safe collection of the finished CNC parts where automated handling is planned.


If you want to optimize production with fixed-head machines, the practical route is to match the machine to the part, reduce unnecessary setups, and use automation where batch size supports it. Rotec’s customer-focused model also adds CAD/CAM, rapid prototyping, assembly, and stock holding, which helps link machining to the wider manufacturing flow.


Supported Operations and Live Tooling Possibilities

Fixed head turning can do far more than simple outside diameter work. With live tooling and mill/turn capability, one machine can complete different operations during the same turning process. That reduces part handling and can improve repeatability when features need close positional control.


At Rotec, supported operations include:

  • turning, boring, grooving, drilling, and screw-cutting
  • milling and cross drilling
  • gear cutting and hobbing where the component requires it


This range means fixed-head machines are suitable for complex shapes as well as standard rotational parts. Typical examples include shafts, pins, bolts, fasteners, heatsinks, die-making consumables, and aerospace components. If your part needs several features machined from solid with stable workholding, fixed head machining is often the better fit than trying to split the job into separate second operation stages.


Achievable Tolerances in CNC Fixed Head Turning

Tolerances in CNC fixed head turning describe how closely the finished part matches the expected dimensions on the drawing. In general terms, CNC turning can achieve tight tolerances and high precision when the process is stable, the machine is suitable, and inspection is built in. The exact result always depends on the part, material, and setup.


A common challenge with fixed-head CNC lathes appears when the maximum length of the part becomes too great relative to its diameter. At that point, deflection, chatter, and vibration at the far end can affect cutting parameters and accuracy. For Rotec-specific figures, use this placeholder.


Factors That Influence Tolerance and Accuracy in Turned Parts

Several factors influence whether turned parts meet tight tolerances. Machine rigidity, thermal stability, tooling condition, and secure workholding all play a direct role in high-precision machining. The complexity of the part also matters because extra features, longer unsupported sections, and deeper cuts can increase risk.


The main process influences include:

  • machine rigidity, spindle condition, and thermal control
  • tool choice, tool wear, and tool life across the batch
  • material type, geometry, workholding method, and cutting strategy


Material choice changes the behavior of the cut as well. Fixed head turning can be used with carbon steel, mild steel, copper, brass, and aluminum, among other suitable materials from a broad range of materials. In-process checks and final CMM inspection are then used to confirm the part against specification. Where company-specific performance data is required, the correct placeholder remains [INSERT ROTEC TOLERANCE FIGURES HERE].


Mapping Best Use Cases: Applications, Parts, and Industries for Fixed Head Turning

Fixed head turning is best suited to short workpieces, larger diameters, and parts that benefit from stable machining and efficient stock removal. It is often the best choice when the component is too short to need guide bush support or when rough bar stock and billet machining are required. That is why it remains common across many industry sectors.


Compared with a sliding head, a fixed head is less suitable for very long, slender components often linked with medical manufacturing and similar applications. Instead, it fits general parts, structural features, and turned components used in aerospace, automotive, oil and gas, rail, and other production environments. The table below maps the common use cases more clearly.


Typical Components and Industry Applications (with Table)

The parts best suited for fixed head turning are usually rigid, relatively short, and practical to machine from bar or billet. They often include features added by turning, milling, drilling, or screw-cutting in one cycle. This makes the process useful across a broad range of materials and production volumes.


Use case Typical components Industries served
High-volume small turned parts pins, shafts, fasteners, bolts automotive, industrial, rail, agricultural
Prototype and low-volume work aerospace components, development parts aerospace, space and satellite, motorsport
Die making consumables stripper and support pins, dies, punches tooling and die-making supply chains
Larger diameter short workpieces cuffs, axles, large pipe connectors oil and gas, automotive, industrial
Functional multi-feature parts heatsinks, hydraulic components, gear-cut parts industrial, military, and general engineering

Medical manufacturing often leans towards sliding head for long, narrow parts, so it is better treated as a contrast case than a core fixed head application here. For Rotec, the strongest fit is with sectors already served from Evesham, UK, using fixed head capability as part of a wider machining service.


Conclusion

In conclusion, fixed head turning is a highly efficient method for producing precision components across various industries, notably the aerospace and automotive sectors. This process excels in creating high-volume small-turned parts and low-volume prototypes, catering to a wide array of applications. With advanced machinery and automation at Rotec Aerospace Limited, we ensure high-quality outputs while meeting stringent tolerances. For a comprehensive quote tailored to your project needs, please send your drawings or CAD files to Sales@rotec-ltd.com or call us at 01386 424111. We look forward to collaborating with you on your precision engineering projects.


Frequently Asked Questions


What is fixed head turning in CNC machining?

Fixed head turning is a turning process on CNC lathes where the main spindle stays in a fixed position while the workpiece rotates and the tools cut it. It is widely used for high-precision parts, especially short components, larger-diameter work, and jobs needing stable machining conditions.


How do I choose between fixed-head and sliding-head CNC for a new project?

Choose a fixed head when the part is short, relatively rigid, or larger in diameter, and choose a sliding head for long, slender parts needing guide bush support. The key differences between these head lathes come from workpiece support, maximum bar diameter, and the practical limits of each type of CNC turning.


How to align headstock to ways on 10F?

Headstock alignment on specific CNC lathes, such as a 10F, depends on the machine builder’s method and service data. As a general rule, alignment should follow the OEM procedure for that headstock and those machine tools, because errors can affect linear rails, geometry, and the expected dimensions of finished parts.


Has anything crazy happened to you this past month?

A better way to frame this for a manufacturing buyer is to ask about unusual production challenges. In precision machining, fast changes in customer requirements, urgent turnaround times, and the need for unique tooling fixtures are common. Rotec plans around those pressures with automated CNC lathes and flexible production capacity.


What is the headstock of a CNC lathe?

The headstock of a CNC lathe is the assembly that houses the main spindle and the drive system. On CNC lathes, it is the part of the machine tools that holds and rotates the raw material 
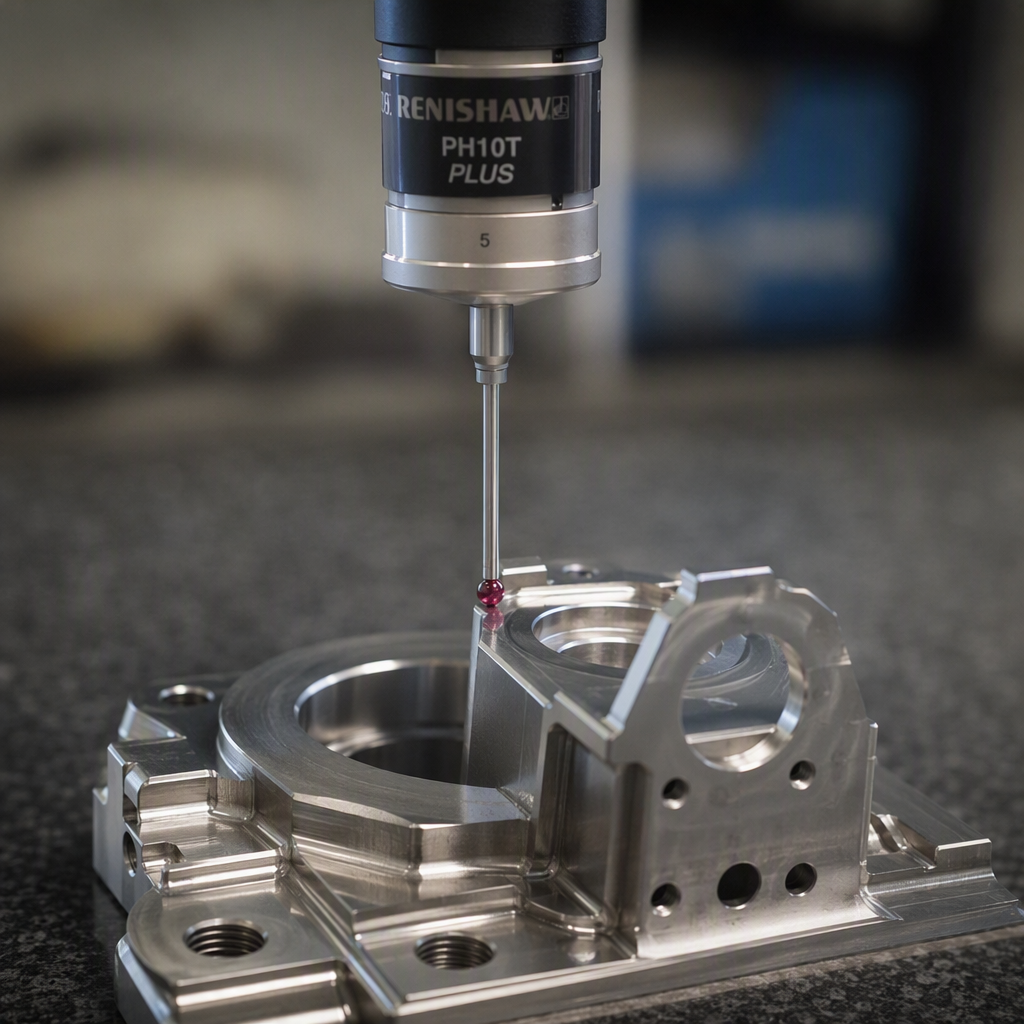

CMM Inspection Explained: Ensuring Precision in CNC Machining
By Will Butler • September 23, 2026
Learn how CMM inspection ensures precision in CNC machining, improves quality control, and verifies critical part dimensions with ROTEC.
Sliding Head vs Fixed Head Turning
By Will Butler • September 14, 2026
Compare sliding head vs fixed head turning to choose the right CNC machining process based on part size, tolerance, complexity, batch size, and cost.
By Jake Hughes • September 9, 2026
Key Highlights Sliding head turning supports bar stock at the cut using a guide bushing and sliding headstock. A CNC Swiss lathe is ideal for small, slender, complex parts needing high precision. It can combine turning, drilling, milling, and threading in one setup. This process helps control vibration and maintain tight tolerances on difficult geometries. Rotec runs 24 automated sliding head machines for prototype work and production volumes. Industries include aerospace, motorsport, military, rail, automotive, and industrial manufacturing. Introduction If you are comparing CNC suppliers for small, detailed parts, sliding head turning deserves close attention. This form of Swiss machining is built for precision components that are hard to machine on standard equipment. It uses a different method from regular CNC turning, giving better support to slender material during cutting. That matters when accuracy, repeatability, and fewer secondary operations affect cost, lead time, and part quality. The next sections explain how it works and when it makes sense. Sliding Head Turning Explained: What Is It and Why Does It Matter? A sliding head or Swiss-type CNC lathe feeds bar stock through a guide point near the tool instead of holding the work far back in a chuck. That simple change gives the process far better control on small, long, or detailed parts. In practice, a Swiss machine is used for complex components that need exceptional accuracy, stable repeatability, and efficient production. A CNC Swiss lathe is especially useful when you need high volumes, fine features, and fewer handoffs between machines. To understand why, it helps to start with the basic definition. Definition of Sliding Head (Swiss-Type) Turning Sliding head turning is a form of CNC turning designed for small, precise work made from bar stock. The machine uses a sliding headstock that moves the material along the Z axis while the tools cut very close to the support point. This differs from a conventional lathe, where the headstock stays fixed. The key part is the guide bushing. It supports the rotating material near the cutting zone, so the section being machined acts more like a short, stiff piece than a long, flexible bar. That reduces vibration, chatter, and bending during machining. Because of this layout, a Swiss machine is well suited to slim, detailed parts with tight dimensional control. Modern versions can also add milling, drilling, and threading in the same cycle, which helps reduce extra handling and improves consistency from part to part. Key Facts at a Glance: Capabilities and Applications At a glance, sliding head turning is built for small parts that need close control and repeat output. It is commonly used when standard turning struggles with part length, feature density, or tolerance demands. That makes it a strong choice for complex components in repeat manufacture. Rotec applies this process across sectors that need dependable quality and traceability. Its sliding head capability supports both sample work and high volumes, depending on the part and batch requirement. Best for small, slender, and complex parts with tight tolerance needs. A CNC Swiss lathe can combine several operations in one cycle. It is widely used where exceptional precision and repeatability matter. Suitable for prototype batches as well as high volumes. Common sectors include aerospace, space & satellite, motorsport, military, rail, and automotive. How Does a Sliding Head (Swiss-Type) CNC Lathe Work? A sliding head machine works by feeding material through a guide bush while the cutting tools stay close to the support point. The CNC Swiss lathe controls spindle movement, tool position, and feed with programmed accuracy, which is why Swiss turning is so effective on slender components. Unlike a fixed-head setup, the sliding headstock moves the bar itself. That reduces unsupported length during cutting and helps protect accuracy. To see how this happens, focus on the two core features first: the headstock and the guide bush. The Sliding Headstock and Guide Bush: Core Features The sliding headstock is what gives the process its name. Instead of spinning a part in one fixed position, the machine pushes or pulls bar material through the work zone. The cutting tool stays near the support point, so the tool is not trying to machine a long unsupported section. That support comes from the guide bush, sometimes called a guide bushing. It sits very close to the tool and holds the material steady as it rotates. This helps reduce deflection, vibration, and chatter, which are common problems on thin workpieces. For you, the result is practical. A properly set guide bush helps the machine hold high precision, better concentricity, and tighter tolerances on long or narrow forms. It also supports consistent surface quality across repeat runs, especially where a standard turning method may struggle. Bar Feed, Spindles, and Multi-Axis Machining A Swiss-type machine is not only about the guide system. It also relies on steady bar feed, spindle coordination, and strong CNC control. Bar feeders keep raw bar stock moving into the machine, which supports longer unattended runs and better output on repeat orders. The main spindle rotates and feeds the material. On more advanced equipment, a subspindle takes the part for back-working operations. This handoff lets the machine finish features on both ends without moving the part to another machine, which saves time and reduces alignment risk. Multi-axis machining adds another layer of capability. Rotec’s sliding head lathes can achieve up to 39 machining positions across 8 axes, often completing a component in a single setup. Its SR-32JIII Type B includes twin spindles, 3 turrets, 36 driven tools, 72 turning tools, and an automatic bar feed up to 42 mm diameter. What Makes Swiss-Type Turning Different from Fixed Head Turning? The main difference is where the workpiece is supported during cutting. In a fixed head lathe, the part is held at one end and the tool moves along it. In Swiss turning, the material passes through a support point near the tool, which changes how the part behaves under load. That design gives better control on small, slender shapes and complex geometries. Conventional lathes still make sense for larger diameters, heavier cuts, and faster job changes. The clearest way to compare both options is side by side. Comparison Table: Sliding Head vs. Fixed Head CNC Turning If you are deciding between processes, look at support method, part geometry, and setup economics. A sliding headstock machine is designed for small, long, detailed work. A fixed head lathe is often the better fit for larger, less slender parts. In short, Swiss-type CNC turning wins when geometry and accuracy are difficult. Standard CNC turning stays valuable where the speed of setup and larger-diameter capacity matter more. When to Choose Sliding Head or Fixed Head for Your Parts Choosing the right process depends on part size, shape, tolerance, and batch volume. Sliding head turning is usually the better option for parts under roughly 32 mm, especially when the length is more than three times the diameter and the drawing calls for close control. Fixed head turning is often better for larger diameters, simpler forms, or low-volume work that needs quick changeovers. The choice is not about which machine is better overall. It is about which machine suits your part with the least waste and risk. Consider sliding head turning when you need: Complex parts with several features completed in a single setup Better surface finishes and less part movement between operations Cost savings by reducing secondary operations Repeat batches where setup time is spread across more parts Advantages of Sliding Head Turning for Precision Engineering For precision machining, the biggest advantages are control, repeatability, and process consolidation. Sliding head turning supports the material where it is cut, which helps maintain high accuracy on features that may be unstable on a standard lathe. That is why it is widely used for tight tolerances on small components. There is also a production benefit. By combining several operations on one machine, you can reduce handling, shorten lead time, and lower waste. The next two sections break those gains into accuracy first, then faster cycle times and automation. Exceptional Accuracy and Tight Tolerances Accuracy starts with stability. In sliding head turning, the guide bush supports the material close to the cutting point, so the bar is less likely to bend away from the tool. That matters when you need narrow diameters, long lengths, or fine feature placement. This setup improves dimensional control and helps the machine deliver high accuracy with less chatter. Production tolerances down to about plus or minus 0.005 mm are routinely associated with this process on suitable work. It also supports better concentricity and cleaner repeat results over longer runs. For buyers and engineers, that means exceptional precision with fewer surprises during inspection. The process is especially valuable where consistent quality matters across many parts, not just the first few off the machine. It is one reason sliding head turning remains a strong choice for demanding precision work. Reduced Cycle Times and Automated Production Speed in this process comes from doing more without stopping. A well-configured machine can turn, drill, mill, groove, bore, screw-cut, and cross-drill in one cycle. That cuts down transfers, queue time, and waiting between separate operations. Automated bar feeding also supports longer, more stable runs. With modern cnc control, main spindle and subspindle work can be coordinated to reduce idle time, which helps deliver faster cycle times on complex repeat parts. This is where Swiss-type turning often becomes more economical than conventional methods. Rotec has built its service around that model. It operates 24 fully automated sliding head machines running around the clock, with staffed hours Monday to Friday, 7:30 am to 5 pm. That automated production approach supports both high volumes and practical cost savings without compromising repeatability. What Can You Make with Swiss-Type Sliding Head Lathes? Swiss-type sliding head lathes are used to make small, detailed, often cylindrical parts that need close control and repeat consistency. They are especially strong on slender parts and complex parts that combine turned and milled features in a compact envelope. Because the process supports a wide range of materials and several operations in one cycle, it suits many precision machining requirements. The best way to judge fit is to look at part size first, then the industries where these complex components are most common. Typical Part Types and Component Size Ranges Swiss turning is best known for small parts with long, narrow proportions and precise features. Typical examples include pins, fasteners, fittings, connectors, injector parts, and other cylindrical items with threads, flats, holes, or back-end details. Medical examples often include dental implants and bone screws. From the compiled process data, Swiss machining commonly handles bar diameters of roughly 2 mm to 38 mm, with some machines reaching larger capacities. Rotec states a practical component size range from as small as 1 mm diameter up to 50 mm diameter, depending on the application and machine used. That range is important if your part sits near the limits of standard turning. Small parts with complex features, long unsupported lengths, or strict tolerance needs often move toward sliding head technology because it offers better control where conventional turning becomes less stable. Industries Served: Aerospace, Automotive, Medical, and More The process is used across industries that need small, repeatable parts with close dimensional control. In the broader market, that includes aerospace , automotive , medical devices, and electronic components. Typical products include fasteners, fittings, connectors, and detailed valve or sensor parts. Rotec serves a wide industrial spread with sliding head machining. Its quality systems include ISO 9001:2015 and AS9100, which matter to buyers who need formal process control and traceability for precision supply. Examples of sectors served include: Aerospace, Space & Satellite, and Military Formula 1/Motorsport and Automotive Oil & Gas, Agricultural, and Rail Industrial manufacturing, where small repeat components and consistent output are essential Beginner’s Guide: Getting Started with Sliding Head Turning If you are new to Swiss CNC machining , start with the basics: the machine, the material, and the setup logic. A sliding head process depends heavily on correct bar stock, stable tooling, guide bush adjustment, and sound programming. It is more specialized than general turning, so preparation matters. That does not mean it is hard to understand. It means each stage must be controlled carefully. The next sections cover the essential equipment, then the step-by-step flow from material preparation through machining and quality checks. Essential Equipment, Resources, and Setup for Swiss-Type Machining A Swiss-type machine tool needs more than the lathe itself. You also need suitable bar feeders, correctly sized collets, a properly adjusted guide bush, and tooling that matches the part geometry and material. Since the bar runs through the support system, straightness and diameter consistency are critical from the start. The CNC lathe must also be configured for the planned sequence of operations. That includes spindle setup, tool positions, and any back-working steps. Tooling options may include turning tools, drilling tools, milling tools, and thread tools, depending on the part. For more advanced production, machine capability matters a lot. Rotec’s fleet includes Star sliding head machines, with four additional Star machines added in 2021. Continual investment like this helps maintain capability for both simple repeat parts and more complex, multi-operation work. Step-by-Step Process for Using a Sliding Head CNC Lathe The machining process follows a clear order, even though the machine itself is complex. First the material is prepared, then the guide system and tools are set, then the program is proved out, and finally the cycle is run with checks for part quality and tool condition. A CNC Swiss lathe works best when each stage is planned around part geometry, feature order, and chip control. Because many parts are completed in a single setup, small mistakes early in the process can affect the full cycle. The basic flow usually includes: Prepare bar stock and confirm material condition Set the machine, guide bush, and tooling positions Program operations and verify spindle timing Run the part, monitor tool wear, and inspect surface finishes Step 1: Preparing Your Bar Stock and Materials Everything starts with the right raw material. In sliding head work, bar stock must be consistent in size and straightness because it passes through the guide system during machining. Poor material quality can lead to chatter, extra wear, and dimensional drift. This process can handle a wide range of materials, but the exact grade affects speeds, chip formation, and coolant needs. Common examples from the compiled data include stainless steel, carbon steel, brass, aluminum, titanium, nickel alloys, copper, and engineering plastics. Each behaves differently at the tool tip. Material preparation is not only about selecting the grade. You also need to confirm bar diameter, straightness, and suitability for the guide bush. For guide-bushing work, centerless-ground stock with tight diameter control is commonly preferred because it supports stable running and predictable results. Step 2: Setting Up the Sliding Head Lathe and Guide Bush Setup on a sliding head lathe is more involved than on many standard turning machines. The machine tool must be prepared with the correct collet, tool arrangement, and guide bush setting before any production cycle begins. This stage has a strong effect on accuracy and stability. The guide bush needs the right clearance. Too tight, and the bar may galle or run poorly. Too loose, and the material loses the support that makes the process effective. Good setup keeps the cutting zone stable and protects both part quality and tool life. On any CNC lathe, correct alignment matters. On a Swiss-type machine, it matters even more because many operations are happening in a compact area. Careful setup helps prevent taper, chatter marks, drifting concentricity, and premature wear across the run. Step 3: Programming the CNC Machine for Multi-Axis Operations Programming a CNC Swiss lathe means planning movement, timing, and feature order very carefully. The CNC control must coordinate bar feed, spindle motion, tool changes, and any handoff to a sub-spindle. When live tooling is involved, the program also has to manage milling, drilling, or cross-hole features within the same cycle. This is why beginners should focus on sequence first. Multi-axis machining creates efficiency, but only when the operation order supports stable cutting and safe part transfer. Programs are often tested with simulation or prove-out runs to catch collisions and wasted motion before production begins. Complex geometries benefit most from this approach. A well-written program can complete front-end and back-end features without moving the component to another machine. That reduces handling risk and supports better repeatability across finished batches. Step 4: Running the Machining Cycle and Quality Checks Once the setup and program are proven, the machining process moves into production. Even with automation, the cycle still needs control. Operators watch spindle behavior, chip flow, part handoff, and machine condition to confirm everything stays stable through the run. Quality checks are essential because small changes can affect many parts quickly. In sliding head work, worn tools, poor material behavior, or drifting bush conditions may show up as taper, chatter, or size variation. Monitoring tool wear early helps avoid large scrap batches during unattended running. Good control supports exceptional surface finishes and repeat dimensions. It also builds consistent quality from first-off approval through the rest of the order. For buyers, that matters just as much as speed, because reliable output reduces inspection issues, rework, and delivery risk. Materials and Features: What Swiss-Type CNC Lathes Can Handle Swiss-type machines are versatile, but they are not material-blind. The process can machine a wide range of materials, yet bar quality, chip control, and tool selection strongly affect the result. That is especially true in CNC machining, where small features and long runs leave little room for variation. The process also handles more than plain turning. With the right cutting tool and machine configuration, it can produce complex parts with strong surface finishes while combining several operations in one cycle. The next sections cover materials first, then multi-process capability. Compatible Metals, Plastics, and Alloys Swiss-type turning can process many common engineering materials as long as they are suitable for bar-fed machining. From the compiled information, typical groups include free-cutting steels, stainless steel grades, brass, copper, aluminum, titanium, cobalt and nickel alloys, and engineering plastics such as PEEK, nylon, and acetal. The material choice affects chip formation, cutting speed, tool wear, and thermal behavior. Stainless steel and tougher alloys may need closer control, while brass and some free-cutting steels are often easier to machine. Plastics also work well, though heat must be watched to protect shape and finish. For best results, the bar stock itself must be consistent. Straightness and diameter control matter because the material passes through the guide system. When those basics are right, the process can deliver exceptional accuracy across a broad range of turned and milled part features. Machining Multiple Processes in One Setup One of the biggest strengths of this technology is process consolidation. A modern sliding head machine can combine turning, drilling, milling, grooving, boring, screw-cutting, and cross-drilling in a single setup. That means the part can often leave the machine close to complete. Live tooling and subspindle capability make this possible. Instead of moving the component between several machines, the process keeps work in one controlled cycle. That reduces alignment risk, handling time, and inspection issues linked to multiple transfers. There are limits, though. Setup takes longer, the machines are more specialized, and material quality matters more than on general turning equipment. Still, for complex parts that would otherwise need many secondary operations, the reduction in extra handling can create real cost savings and more stable repeat production. Conclusion In conclusion, sliding head (Swiss-type) turning is a game-changer in precision engineering, offering unmatched versatility and efficiency. With its ability to perform multiple operations in one setup, this machining method excels in producing intricate parts with tight tolerances across various industries, including aerospace and automotive. By understanding its capabilities and processes, you can make informed decisions that enhance production quality and reduce cycle times. If you're ready to explore how sliding head turning can benefit your projects, reach out to us for a free consultation and discover tailored solutions that meet your specific needs. Frequently Asked Questions What is the difference between sliding head and fixed head turning? The main difference is support during the machining process. A sliding headstock pushes material through a guide bushing near the cut, while a fixed head lathe holds the work at one end. That gives sliding head turning better control on slender parts than conventional CNC turning. What size parts can Swiss turning machines make? A CNC Swiss lathe is mainly used for small parts and slender parts made from bar stock. Compiled process guidance often places the range around 2 mm to 38 mm diameter, while Rotec states capability from 1 mm up to 50 mm diameter, depending on application and machine. Is sliding head turning the same as Swiss turning? Yes. Swiss turning and sliding head turning are different names for the same core CNC turning method. The process uses a sliding headstock and guide support to machine small precision components accurately. Today, a modern Swiss machine can also mill, drill, and thread within the same cycle. How does the guide bush improve machining accuracy? The guide bushing supports the material very close to the tool, which reduces bending and vibration during cutting. That helps the machine maintain high precision, tighter tolerances, and better surface finishes, especially on long or narrow parts where unsupported material would normally deflect.
industrial-cnc-machining
By Brick Digital • October 30, 2024
Discover how CNC horizontal milling machines work, their key components, and why they suit complex, high-volume parts. Read Rotec's full guide.
industrial-cnc-machining
By Brick Digital • September 30, 2024
Learn how CNC plasma cutting works, its main components, industry applications, and how it compares to laser and traditional cutting methods.
cnc-machinig
By Brick Digital • August 30, 2024
Explore the main types of CNC turning tools, how to choose the right one for your material, and tips to boost precision and tool life.
oig-cnc-sercice
By Brick Digital • July 22, 2024
Understand how CNC production machining enables high-volume, precision part manufacturing and the technologies driving modern efficiency.
industrial-cnc-machining
By Brick Digital • June 28, 2024
See how robotic CNC machining combines automation and precision engineering to boost speed, accuracy and output across manufacturing.
cnc-machining
By Jake Hughes • June 24, 2024
Practical tips to lower CNC machining costs—from material choice to design optimization—without compromising precision or quality.
oig-cnc-sercice
By Jake Hughes • June 24, 2024
Compare aluminium, stainless steel, brass, copper and titanium to find the most cost-effective material for your next CNC project.