The Evolution and Applications of CNC Technology ~

Brick Digital • January 30, 2024

Computer Numerical Control (CNC) machining has revolutionised the manufacturing landscape, becoming a cornerstone of modern industry.

CNC machining involves the use of computerised systems to control and manipulate tools for precision machining of various materials. The impact of CNC technology is profound, enabling unparalleled levels of accuracy, efficiency, and customisation in manufacturing processes. To fully appreciate its significance, we need to look at the pivotal moments and technological breakthroughs that have shaped the foundation for CNC technology, exploring the milestones, challenges, and innovations that have defined this transformative field.


If you want to learn more about how CNC machining has evolved over the decades to get to where it is now, you have come to the right page! In this article, we will delve into the fascinating history of CNC machining, tracing its evolution from rudimentary numerical control systems to the sophisticated and interconnected CNC systems of today. Not only that, we will also have a look at the ongoing technological advancements and what the future holds for this groundbreaking technology. Without further ado, let's dive right in!


Evolution of CNC Technology Over Decades


1950s - Early Concepts and Precursors


Development of Numerical Control (NC) Systems:
In the 1950s, the groundwork for CNC machining was laid with the development of numerical control systems. Engineers and researchers explored ways to automate machining processes, setting the stage for the technological leaps that would follow.


Application in Military and Aerospace Industries:
The military and aerospace sectors played a crucial role in the early adoption of numerical control. CNC technology emerged as a solution to enhance precision and efficiency in manufacturing components for complex aircraft and defence systems.


1960s - First Steps Towards Automation


Punched Tape Systems:
The 1960s witnessed the introduction of punched tape systems, a primitive form of programming for machining operations. While limited, these early automation methods represented a fundamental shift towards more efficient and accurate machining processes.


Limited Programmability, Challenges and Solutions:
Despite advancements, the programmability of early CNC systems was constrained. Engineers faced challenges in programming complex shapes and patterns. However, these limitations spurred further innovation, paving the way for more sophisticated programming languages.


1970s - Birth of CNC Machining


Introduction of Computers to Machining:
The 1970s marked a pivotal moment with the introduction of computers to machining processes. This era saw a transition from analog to digital control, allowing for greater flexibility and precision in machining operations.


Emergence of the Term CNC (Computer Numerical Control):
As computers became integral to machining, the term "Computer Numerical Control" (CNC) was coined to describe this revolutionary approach. CNC represented a paradigm shift in manufacturing, bringing about a new era of automated and computer-driven machining.


Development of the First CNC Machine Tool:
Visionaries like John T. Parsons and the MIT Servomechanisms Laboratory developed the first CNC machine tool during this period. This groundbreaking innovation laid the foundation for the widespread adoption of CNC technology across various industries.


1980s - Transition from Punched Tapes to Computer Programming


Elimination of Punched Tape Limitations:
The 1980s witnessed the gradual phasing out of punched tape systems. This transition allowed for more sophisticated programming methods, eliminating the constraints imposed by punched tape technology.


Integration of Computers in CNC Machining:
The integration of computers in CNC machining became more seamless, leading to improved accuracy and versatility in manufacturing processes. CNC machines evolved to handle complex tasks with greater efficiency.


Early Programming Languages and Advances:
During this period, early programming languages for CNC machining, such as G-code, gained prominence. These languages enabled operators to communicate complex instructions to CNC machines, expanding the scope of achievable shapes and designs.


1990s - Advancements in Control Systems


Open-Loop vs. Closed-Loop Systems:
The 1990s brought advancements in control systems, distinguishing between open-loop and closed-loop CNC systems. Closed-loop systems, incorporating feedback mechanisms, enhanced precision and reliability in machining operations.


Integration of Microprocessors in CNC Machines:
Microprocessor technology became integral to CNC machines, allowing for faster computation and more intricate control. This era marked a significant leap in the overall performance and capabilities of CNC systems.


2000s - Expansion of CNC Applications


CNC Turning and Milling Machines:
The 2000s witnessed a proliferation of CNC applications, with a focus on turning and milling machines. These CNC systems allowed for the precise shaping of raw materials into intricate components, facilitating mass production with unprecedented accuracy.


Multi-Axis Machining Centers:
Advancements in multi-axis machining centres became a hallmark of the 2000s. These machines enabled complex and multi-dimensional machining, expanding the possibilities for intricate part production in industries ranging from automotive to aerospace.


Introduction of Waterjet and Laser Cutting Systems:
CNC technology embraced new frontiers with the introduction of waterjet and laser cutting systems. These technologies allowed for non-traditional machining methods, offering precision in cutting a variety of materials, from metals to composites.


2010s - Software Developments


CAD/CAM Integration for Enhanced Design and Manufacturing:
The 2010s marked a significant emphasis on Computer-Aided Design (CAD) and Computer-Aided Manufacturing (CAM) integration. This synergy between design and manufacturing software streamlined processes, enabling seamless transitions from digital models to physical prototypes.


Simulation and Verification Tools for Precision:
The advent of simulation and verification tools in CNC machining during this decade enhanced precision and minimised errors. Engineers could simulate machining processes virtually, allowing for the identification and correction of potential issues before the physical machining began.


Ongoing Technological Advancements in CNC


High-Speed Machining Techniques:
The 2020s saw a continued focus on high-speed machining techniques. Enhanced spindle speeds and cutting strategies allowed for faster production while maintaining precision, catering to the demands of modern manufacturing.


Internet of Things (IoT) Integration in CNC Machines:
IoT integration became increasingly prevalent in CNC machines. Connected CNC systems facilitated real-time monitoring, predictive maintenance, and data-driven optimisation, contributing to overall efficiency and machine health.


Augmented Reality (AR) and Virtual Reality (VR) Applications in CNC:
The integration of Augmented Reality (AR) and Virtual Reality (VR) applications in CNC machining provided innovative solutions for training, simulation, and maintenance. These technologies enhanced the user experience, making CNC operations more intuitive and accessible.


Future Trends and Anticipated Developments


Additive Manufacturing and CNC Integration:
The synergy between additive manufacturing (3D printing) and CNC machining is anticipated to grow, offering a hybrid approach that combines the benefits of both technologies.


Robotics and Automation in CNC Processes:
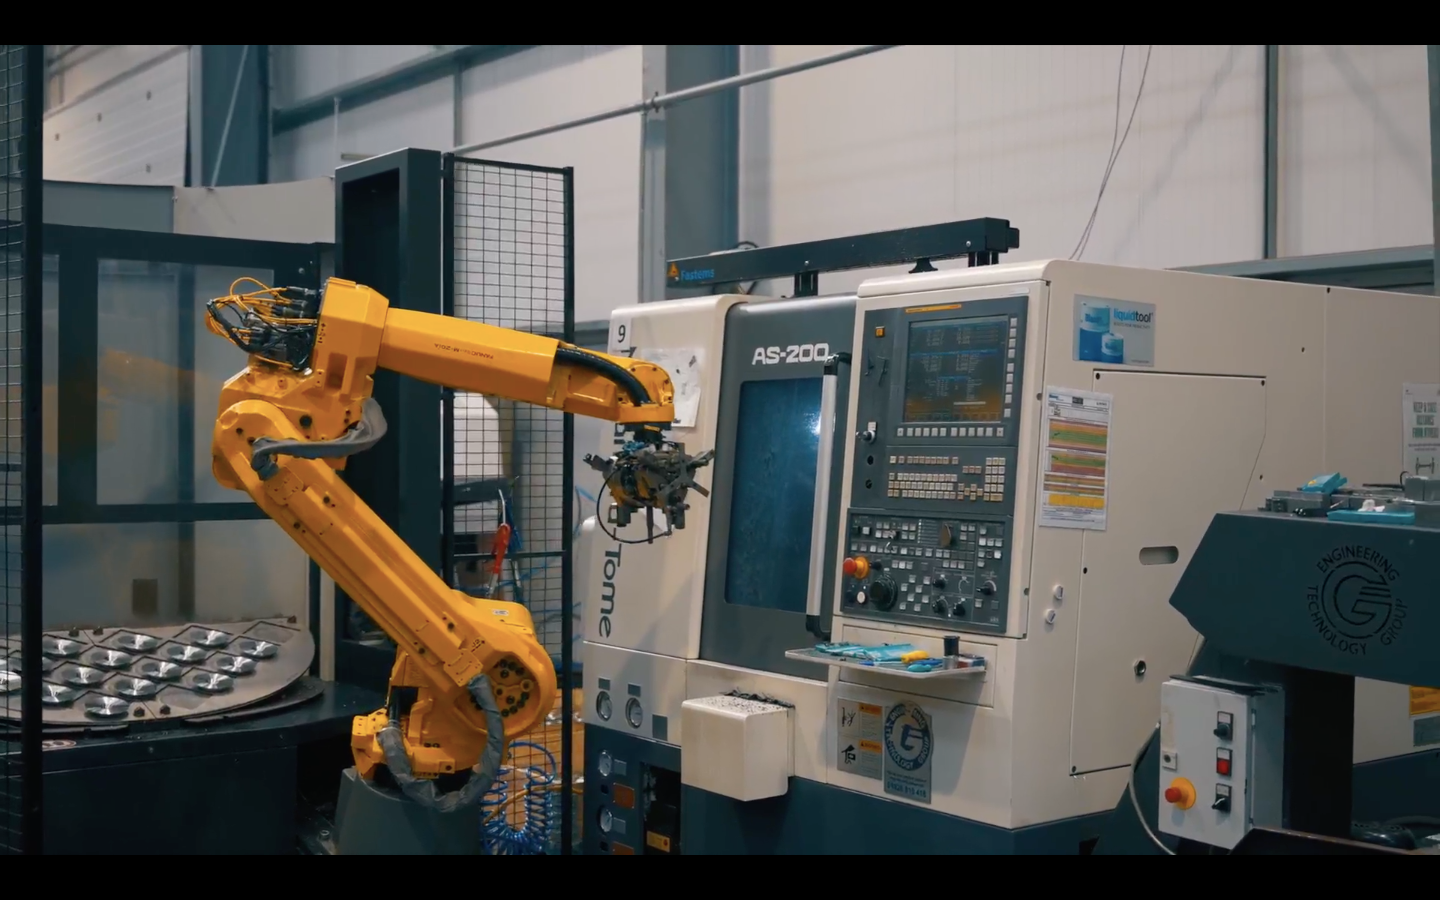
The integration of robotics and automation into CNC processes is expected to increase, further reducing manual intervention, improving efficiency, and enabling lights-out manufacturing.


Sustainable and Green CNC Practices:
Future trends in CNC machining are likely to include a focus on sustainable and environmentally friendly practices. This may involve the adoption of greener materials, energy-efficient machining processes, and waste reduction initiatives.


Impact of CNC Machining on Manufacturing Industries


CNC machining has exerted a transformative influence on manufacturing industries, shaping the way products are conceptualised, designed, and produced. This section explores the profound impact of CNC technology on various facets of manufacturing, illustrating its role in enhancing precision, enabling mass production, and contributing to advancements in critical industries.


Increased Precision and Efficiency


The advent of CNC machining brought a paradigm shift in precision engineering. The ability to program and automate machining processes down to micrometre-level accuracy revolutionised the production of intricate components. CNC machines consistently deliver high precision, reducing errors and ensuring conformity to exact specifications. This precision is especially critical in industries such as aerospace and medical, where tight tolerances are non-negotiable.


Beyond precision, CNC machining significantly improved efficiency. The automation of repetitive tasks eliminated the variability associated with manual operations, resulting in faster production cycles and reduced lead times. This efficiency not only enhances productivity but also contributes to cost-effectiveness in the long run.


Mass Production and Customisation


CNC machining played a pivotal role in the shift from traditional manufacturing to mass production. The ability to reproduce complex components with unparalleled accuracy allowed industries to scale production without compromising quality. This scalability is particularly evident in automotive manufacturing, where CNC technology enables the efficient production of large quantities of standardised parts.


Simultaneously, CNC machining facilitated a paradoxical trend towards customisation. While mass-producing standardised components, CNC machines can swiftly switch between designs, accommodating variations in product specifications. This flexibility has empowered industries to meet the growing demand for customised and specialised products, from personalised medical implants to uniquely designed automotive components.


Small Business and Customisation


CNC for Small and Medium-Sized Enterprises (SMEs)


The accessibility of CNC machines has levelled the playing field for small and medium-sized enterprises. SMEs can harness the power of CNC technology to compete on quality and precision, enabling them to take on projects that were once exclusive to larger corporations.


Having worked closely with small businesses, we have seen firsthand the transformative impact of CNC technology. It's not just about the machines; it's about empowering smaller players to dream big and innovate.


Customisation and Prototyping Services


CNC machining's ability to facilitate rapid prototyping has revolutionised the product development cycle. Whether it's a one-of-a-kind design or a prototype for mass production, CNC's flexibility allows for quick iterations, reducing time-to-market and fostering a culture of innovation.


In the realm of creativity and design,
acrylic CNC machining acts as a versatile tool for turning imaginative concepts into tangible prototypes. It's a game-changer for those pushing the boundaries of what's possible.


Applications Across Industries


CNC machining has found diverse applications across various industries, each benefiting from its unique capabilities.


Electronics and Semiconductors


In the electronics sector, CNC technology is crucial for the precision machining of intricate components on circuit boards. The miniaturisation trend in electronics demands microscopic precision, a feat efficiently achieved by CNC machines. Moreover, CNC machining plays a pivotal role in the production of semiconductor components, contributing to the rapid advancements in technology.


Consumer Goods Manufacturing


CNC machining has permeated the consumer goods manufacturing sector, allowing for the efficient production of products ranging from kitchen appliances to consumer electronics. The ability to seamlessly transition from prototyping to mass production caters to the dynamic nature of consumer preferences and market trends.


Aerospace Industry


CNC machining is indispensable in aerospace manufacturing for its ability to craft precision components crucial for aircraft and spacecraft. From turbine blades to structural components, the aerospace sector relies on CNC technology to meet the stringent demands of high-performance and safety standards.


Automotive Industry


In the automotive sector, CNC machining has become synonymous with efficiency and precision. From engine parts to intricate components in modern vehicles, CNC technology plays a central role in ensuring the reliability and performance of automobiles. Moreover, CNC machines are vital in prototyping and developing new automotive designs.


Medical Industry


In the medical field, CNC machining is instrumental in the production of medical devices, implants, and prosthetics. The ability to create complex and customised components with biocompatible materials has revolutionised medical manufacturing, offering patients tailored solutions and improving the overall quality of healthcare.


As CNC machining continues to evolve, its impact on manufacturing will only deepen. The increased precision, scalability, and flexibility provided by CNC technology have positioned it as a cornerstone of modern industrial processes.


Final Thoughts


From its humble beginnings to its current state as an integral part of industries worldwide, the story of CNC machining evolution is one of ingenuity, adaptability, and the relentless pursuit of manufacturing excellence. Looking ahead, the anticipated trends of additive manufacturing integration, robotics, and sustainable practices signify a future where CNC machining will continue to be a driving force in shaping the manufacturing landscape.


At Rotec, we specialise in turning possibilities into reality, crafting intricate components that redefine industry standards.
Contact us today to explore how our cutting-edge CNC and precision engineering capabilities can support your ongoing or upcoming projects!

Sliding Head vs Fixed Head Turning
By Will Butler September 14, 2026
Compare sliding head vs fixed head turning to choose the right CNC machining process based on part size, tolerance, complexity, batch size, and cost.
By Jake Hughes September 9, 2026
Key Highlights Sliding head turning supports bar stock at the cut using a guide bushing and sliding headstock. A CNC Swiss lathe is ideal for small, slender, complex parts needing high precision. It can combine turning, drilling, milling, and threading in one setup. This process helps control vibration and maintain tight tolerances on difficult geometries. Rotec runs 24 automated sliding head machines for prototype work and production volumes. Industries include aerospace, motorsport, military, rail, automotive, and industrial manufacturing. Introduction If you are comparing CNC suppliers for small, detailed parts, sliding head turning deserves close attention. This form of Swiss machining is built for precision components that are hard to machine on standard equipment. It uses a different method from regular CNC turning, giving better support to slender material during cutting. That matters when accuracy, repeatability, and fewer secondary operations affect cost, lead time, and part quality. The next sections explain how it works and when it makes sense. Sliding Head Turning Explained: What Is It and Why Does It Matter? A sliding head or Swiss-type CNC lathe feeds bar stock through a guide point near the tool instead of holding the work far back in a chuck. That simple change gives the process far better control on small, long, or detailed parts. In practice, a Swiss machine is used for complex components that need exceptional accuracy, stable repeatability, and efficient production. A CNC Swiss lathe is especially useful when you need high volumes, fine features, and fewer handoffs between machines. To understand why, it helps to start with the basic definition. Definition of Sliding Head (Swiss-Type) Turning Sliding head turning is a form of CNC turning designed for small, precise work made from bar stock. The machine uses a sliding headstock that moves the material along the Z axis while the tools cut very close to the support point. This differs from a conventional lathe, where the headstock stays fixed. The key part is the guide bushing. It supports the rotating material near the cutting zone, so the section being machined acts more like a short, stiff piece than a long, flexible bar. That reduces vibration, chatter, and bending during machining. Because of this layout, a Swiss machine is well suited to slim, detailed parts with tight dimensional control. Modern versions can also add milling, drilling, and threading in the same cycle, which helps reduce extra handling and improves consistency from part to part. Key Facts at a Glance: Capabilities and Applications At a glance, sliding head turning is built for small parts that need close control and repeat output. It is commonly used when standard turning struggles with part length, feature density, or tolerance demands. That makes it a strong choice for complex components in repeat manufacture. Rotec applies this process across sectors that need dependable quality and traceability. Its sliding head capability supports both sample work and high volumes, depending on the part and batch requirement. Best for small, slender, and complex parts with tight tolerance needs. A CNC Swiss lathe can combine several operations in one cycle. It is widely used where exceptional precision and repeatability matter. Suitable for prototype batches as well as high volumes. Common sectors include aerospace, space & satellite, motorsport, military, rail, and automotive. How Does a Sliding Head (Swiss-Type) CNC Lathe Work? A sliding head machine works by feeding material through a guide bush while the cutting tools stay close to the support point. The CNC Swiss lathe controls spindle movement, tool position, and feed with programmed accuracy, which is why Swiss turning is so effective on slender components. Unlike a fixed-head setup, the sliding headstock moves the bar itself. That reduces unsupported length during cutting and helps protect accuracy. To see how this happens, focus on the two core features first: the headstock and the guide bush. The Sliding Headstock and Guide Bush: Core Features The sliding headstock is what gives the process its name. Instead of spinning a part in one fixed position, the machine pushes or pulls bar material through the work zone. The cutting tool stays near the support point, so the tool is not trying to machine a long unsupported section. That support comes from the guide bush, sometimes called a guide bushing. It sits very close to the tool and holds the material steady as it rotates. This helps reduce deflection, vibration, and chatter, which are common problems on thin workpieces. For you, the result is practical. A properly set guide bush helps the machine hold high precision, better concentricity, and tighter tolerances on long or narrow forms. It also supports consistent surface quality across repeat runs, especially where a standard turning method may struggle. Bar Feed, Spindles, and Multi-Axis Machining A Swiss-type machine is not only about the guide system. It also relies on steady bar feed, spindle coordination, and strong CNC control. Bar feeders keep raw bar stock moving into the machine, which supports longer unattended runs and better output on repeat orders. The main spindle rotates and feeds the material. On more advanced equipment, a subspindle takes the part for back-working operations. This handoff lets the machine finish features on both ends without moving the part to another machine, which saves time and reduces alignment risk. Multi-axis machining adds another layer of capability. Rotec’s sliding head lathes can achieve up to 39 machining positions across 8 axes, often completing a component in a single setup. Its SR-32JIII Type B includes twin spindles, 3 turrets, 36 driven tools, 72 turning tools, and an automatic bar feed up to 42 mm diameter. What Makes Swiss-Type Turning Different from Fixed Head Turning? The main difference is where the workpiece is supported during cutting. In a fixed head lathe, the part is held at one end and the tool moves along it. In Swiss turning, the material passes through a support point near the tool, which changes how the part behaves under load. That design gives better control on small, slender shapes and complex geometries. Conventional lathes still make sense for larger diameters, heavier cuts, and faster job changes. The clearest way to compare both options is side by side. Comparison Table: Sliding Head vs. Fixed Head CNC Turning If you are deciding between processes, look at support method, part geometry, and setup economics. A sliding headstock machine is designed for small, long, detailed work. A fixed head lathe is often the better fit for larger, less slender parts. In short, Swiss-type CNC turning wins when geometry and accuracy are difficult. Standard CNC turning stays valuable where the speed of setup and larger-diameter capacity matter more. When to Choose Sliding Head or Fixed Head for Your Parts Choosing the right process depends on part size, shape, tolerance, and batch volume. Sliding head turning is usually the better option for parts under roughly 32 mm, especially when the length is more than three times the diameter and the drawing calls for close control. Fixed head turning is often better for larger diameters, simpler forms, or low-volume work that needs quick changeovers. The choice is not about which machine is better overall. It is about which machine suits your part with the least waste and risk. Consider sliding head turning when you need: Complex parts with several features completed in a single setup Better surface finishes and less part movement between operations Cost savings by reducing secondary operations Repeat batches where setup time is spread across more parts Advantages of Sliding Head Turning for Precision Engineering For precision machining, the biggest advantages are control, repeatability, and process consolidation. Sliding head turning supports the material where it is cut, which helps maintain high accuracy on features that may be unstable on a standard lathe. That is why it is widely used for tight tolerances on small components. There is also a production benefit. By combining several operations on one machine, you can reduce handling, shorten lead time, and lower waste. The next two sections break those gains into accuracy first, then faster cycle times and automation. Exceptional Accuracy and Tight Tolerances Accuracy starts with stability. In sliding head turning, the guide bush supports the material close to the cutting point, so the bar is less likely to bend away from the tool. That matters when you need narrow diameters, long lengths, or fine feature placement. This setup improves dimensional control and helps the machine deliver high accuracy with less chatter. Production tolerances down to about plus or minus 0.005 mm are routinely associated with this process on suitable work. It also supports better concentricity and cleaner repeat results over longer runs. For buyers and engineers, that means exceptional precision with fewer surprises during inspection. The process is especially valuable where consistent quality matters across many parts, not just the first few off the machine. It is one reason sliding head turning remains a strong choice for demanding precision work. Reduced Cycle Times and Automated Production Speed in this process comes from doing more without stopping. A well-configured machine can turn, drill, mill, groove, bore, screw-cut, and cross-drill in one cycle. That cuts down transfers, queue time, and waiting between separate operations. Automated bar feeding also supports longer, more stable runs. With modern cnc control, main spindle and subspindle work can be coordinated to reduce idle time, which helps deliver faster cycle times on complex repeat parts. This is where Swiss-type turning often becomes more economical than conventional methods. Rotec has built its service around that model. It operates 24 fully automated sliding head machines running around the clock, with staffed hours Monday to Friday, 7:30 am to 5 pm. That automated production approach supports both high volumes and practical cost savings without compromising repeatability. What Can You Make with Swiss-Type Sliding Head Lathes? Swiss-type sliding head lathes are used to make small, detailed, often cylindrical parts that need close control and repeat consistency. They are especially strong on slender parts and complex parts that combine turned and milled features in a compact envelope. Because the process supports a wide range of materials and several operations in one cycle, it suits many precision machining requirements. The best way to judge fit is to look at part size first, then the industries where these complex components are most common. Typical Part Types and Component Size Ranges Swiss turning is best known for small parts with long, narrow proportions and precise features. Typical examples include pins, fasteners, fittings, connectors, injector parts, and other cylindrical items with threads, flats, holes, or back-end details. Medical examples often include dental implants and bone screws. From the compiled process data, Swiss machining commonly handles bar diameters of roughly 2 mm to 38 mm, with some machines reaching larger capacities. Rotec states a practical component size range from as small as 1 mm diameter up to 50 mm diameter, depending on the application and machine used. That range is important if your part sits near the limits of standard turning. Small parts with complex features, long unsupported lengths, or strict tolerance needs often move toward sliding head technology because it offers better control where conventional turning becomes less stable. Industries Served: Aerospace, Automotive, Medical, and More The process is used across industries that need small, repeatable parts with close dimensional control. In the broader market, that includes aerospace , automotive , medical devices, and electronic components. Typical products include fasteners, fittings, connectors, and detailed valve or sensor parts. Rotec serves a wide industrial spread with sliding head machining. Its quality systems include ISO 9001:2015 and AS9100, which matter to buyers who need formal process control and traceability for precision supply. Examples of sectors served include: Aerospace, Space & Satellite, and Military Formula 1/Motorsport and Automotive Oil & Gas, Agricultural, and Rail Industrial manufacturing, where small repeat components and consistent output are essential Beginner’s Guide: Getting Started with Sliding Head Turning If you are new to Swiss CNC machining , start with the basics: the machine, the material, and the setup logic. A sliding head process depends heavily on correct bar stock, stable tooling, guide bush adjustment, and sound programming. It is more specialized than general turning, so preparation matters. That does not mean it is hard to understand. It means each stage must be controlled carefully. The next sections cover the essential equipment, then the step-by-step flow from material preparation through machining and quality checks. Essential Equipment, Resources, and Setup for Swiss-Type Machining A Swiss-type machine tool needs more than the lathe itself. You also need suitable bar feeders, correctly sized collets, a properly adjusted guide bush, and tooling that matches the part geometry and material. Since the bar runs through the support system, straightness and diameter consistency are critical from the start. The CNC lathe must also be configured for the planned sequence of operations. That includes spindle setup, tool positions, and any back-working steps. Tooling options may include turning tools, drilling tools, milling tools, and thread tools, depending on the part. For more advanced production, machine capability matters a lot. Rotec’s fleet includes Star sliding head machines, with four additional Star machines added in 2021. Continual investment like this helps maintain capability for both simple repeat parts and more complex, multi-operation work. Step-by-Step Process for Using a Sliding Head CNC Lathe The machining process follows a clear order, even though the machine itself is complex. First the material is prepared, then the guide system and tools are set, then the program is proved out, and finally the cycle is run with checks for part quality and tool condition. A CNC Swiss lathe works best when each stage is planned around part geometry, feature order, and chip control. Because many parts are completed in a single setup, small mistakes early in the process can affect the full cycle. The basic flow usually includes: Prepare bar stock and confirm material condition Set the machine, guide bush, and tooling positions Program operations and verify spindle timing Run the part, monitor tool wear, and inspect surface finishes Step 1: Preparing Your Bar Stock and Materials Everything starts with the right raw material. In sliding head work, bar stock must be consistent in size and straightness because it passes through the guide system during machining. Poor material quality can lead to chatter, extra wear, and dimensional drift. This process can handle a wide range of materials, but the exact grade affects speeds, chip formation, and coolant needs. Common examples from the compiled data include stainless steel, carbon steel, brass, aluminum, titanium, nickel alloys, copper, and engineering plastics. Each behaves differently at the tool tip. Material preparation is not only about selecting the grade. You also need to confirm bar diameter, straightness, and suitability for the guide bush. For guide-bushing work, centerless-ground stock with tight diameter control is commonly preferred because it supports stable running and predictable results. Step 2: Setting Up the Sliding Head Lathe and Guide Bush Setup on a sliding head lathe is more involved than on many standard turning machines. The machine tool must be prepared with the correct collet, tool arrangement, and guide bush setting before any production cycle begins. This stage has a strong effect on accuracy and stability. The guide bush needs the right clearance. Too tight, and the bar may galle or run poorly. Too loose, and the material loses the support that makes the process effective. Good setup keeps the cutting zone stable and protects both part quality and tool life. On any CNC lathe, correct alignment matters. On a Swiss-type machine, it matters even more because many operations are happening in a compact area. Careful setup helps prevent taper, chatter marks, drifting concentricity, and premature wear across the run. Step 3: Programming the CNC Machine for Multi-Axis Operations Programming a CNC Swiss lathe means planning movement, timing, and feature order very carefully. The CNC control must coordinate bar feed, spindle motion, tool changes, and any handoff to a sub-spindle. When live tooling is involved, the program also has to manage milling, drilling, or cross-hole features within the same cycle. This is why beginners should focus on sequence first. Multi-axis machining creates efficiency, but only when the operation order supports stable cutting and safe part transfer. Programs are often tested with simulation or prove-out runs to catch collisions and wasted motion before production begins. Complex geometries benefit most from this approach. A well-written program can complete front-end and back-end features without moving the component to another machine. That reduces handling risk and supports better repeatability across finished batches. Step 4: Running the Machining Cycle and Quality Checks Once the setup and program are proven, the machining process moves into production. Even with automation, the cycle still needs control. Operators watch spindle behavior, chip flow, part handoff, and machine condition to confirm everything stays stable through the run. Quality checks are essential because small changes can affect many parts quickly. In sliding head work, worn tools, poor material behavior, or drifting bush conditions may show up as taper, chatter, or size variation. Monitoring tool wear early helps avoid large scrap batches during unattended running. Good control supports exceptional surface finishes and repeat dimensions. It also builds consistent quality from first-off approval through the rest of the order. For buyers, that matters just as much as speed, because reliable output reduces inspection issues, rework, and delivery risk. Materials and Features: What Swiss-Type CNC Lathes Can Handle Swiss-type machines are versatile, but they are not material-blind. The process can machine a wide range of materials, yet bar quality, chip control, and tool selection strongly affect the result. That is especially true in CNC machining, where small features and long runs leave little room for variation. The process also handles more than plain turning. With the right cutting tool and machine configuration, it can produce complex parts with strong surface finishes while combining several operations in one cycle. The next sections cover materials first, then multi-process capability. Compatible Metals, Plastics, and Alloys Swiss-type turning can process many common engineering materials as long as they are suitable for bar-fed machining. From the compiled information, typical groups include free-cutting steels, stainless steel grades, brass, copper, aluminum, titanium, cobalt and nickel alloys, and engineering plastics such as PEEK, nylon, and acetal. The material choice affects chip formation, cutting speed, tool wear, and thermal behavior. Stainless steel and tougher alloys may need closer control, while brass and some free-cutting steels are often easier to machine. Plastics also work well, though heat must be watched to protect shape and finish. For best results, the bar stock itself must be consistent. Straightness and diameter control matter because the material passes through the guide system. When those basics are right, the process can deliver exceptional accuracy across a broad range of turned and milled part features. Machining Multiple Processes in One Setup One of the biggest strengths of this technology is process consolidation. A modern sliding head machine can combine turning, drilling, milling, grooving, boring, screw-cutting, and cross-drilling in a single setup. That means the part can often leave the machine close to complete. Live tooling and subspindle capability make this possible. Instead of moving the component between several machines, the process keeps work in one controlled cycle. That reduces alignment risk, handling time, and inspection issues linked to multiple transfers. There are limits, though. Setup takes longer, the machines are more specialized, and material quality matters more than on general turning equipment. Still, for complex parts that would otherwise need many secondary operations, the reduction in extra handling can create real cost savings and more stable repeat production. Conclusion In conclusion, sliding head (Swiss-type) turning is a game-changer in precision engineering, offering unmatched versatility and efficiency. With its ability to perform multiple operations in one setup, this machining method excels in producing intricate parts with tight tolerances across various industries, including aerospace and automotive. By understanding its capabilities and processes, you can make informed decisions that enhance production quality and reduce cycle times. If you're ready to explore how sliding head turning can benefit your projects, reach out to us for a free consultation and discover tailored solutions that meet your specific needs. Frequently Asked Questions What is the difference between sliding head and fixed head turning? The main difference is support during the machining process. A sliding headstock pushes material through a guide bushing near the cut, while a fixed head lathe holds the work at one end. That gives sliding head turning better control on slender parts than conventional CNC turning. What size parts can Swiss turning machines make? A CNC Swiss lathe is mainly used for small parts and slender parts made from bar stock. Compiled process guidance often places the range around 2 mm to 38 mm diameter, while Rotec states capability from 1 mm up to 50 mm diameter, depending on application and machine. Is sliding head turning the same as Swiss turning? Yes. Swiss turning and sliding head turning are different names for the same core CNC turning method. The process uses a sliding headstock and guide support to machine small precision components accurately. Today, a modern Swiss machine can also mill, drill, and thread within the same cycle. How does the guide bush improve machining accuracy? The guide bushing supports the material very close to the tool, which reduces bending and vibration during cutting. That helps the machine maintain high precision, tighter tolerances, and better surface finishes, especially on long or narrow parts where unsupported material would normally deflect.
industrial-cnc-machining
By Brick Digital October 30, 2024
Discover how CNC horizontal milling machines work, their key components, and why they suit complex, high-volume parts. Read Rotec's full guide.
industrial-cnc-machining
By Brick Digital September 30, 2024
Learn how CNC plasma cutting works, its main components, industry applications, and how it compares to laser and traditional cutting methods.
cnc-machinig
By Brick Digital August 30, 2024
Explore the main types of CNC turning tools, how to choose the right one for your material, and tips to boost precision and tool life.
oig-cnc-sercice
By Brick Digital July 22, 2024
Understand how CNC production machining enables high-volume, precision part manufacturing and the technologies driving modern efficiency.
industrial-cnc-machining
By Brick Digital June 28, 2024
See how robotic CNC machining combines automation and precision engineering to boost speed, accuracy and output across manufacturing.
cnc-machining
By Jake Hughes June 24, 2024
Practical tips to lower CNC machining costs—from material choice to design optimization—without compromising precision or quality.
oig-cnc-sercice
By Jake Hughes June 24, 2024
Compare aluminium, stainless steel, brass, copper and titanium to find the most cost-effective material for your next CNC project.
robotic-cnc-machining
By Jake Hughes June 24, 2024
Learn what robotic CNC machining is, how it works, its benefits and how automation improves precision, productivity, and manufacturing efficiency.